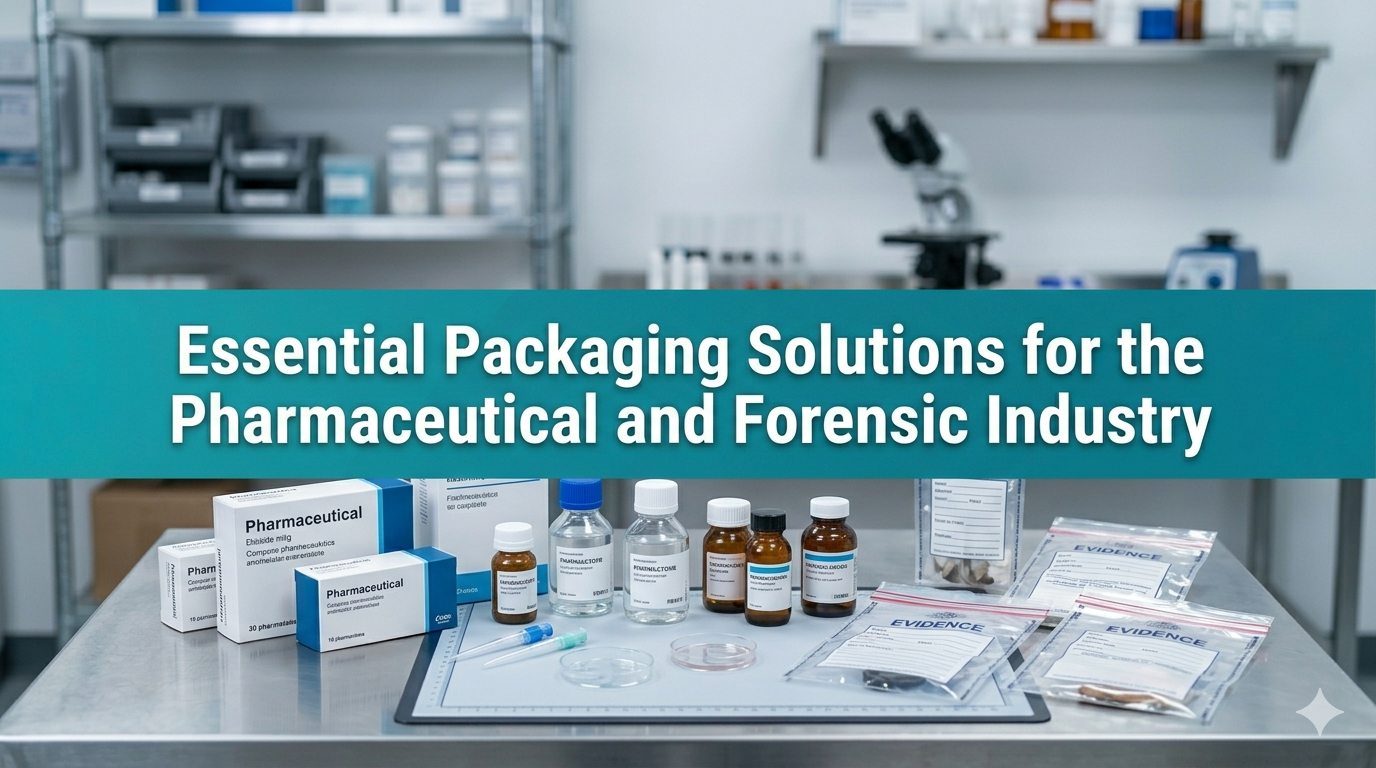
Essential Packaging Solutions for the Pharmaceutical and Forensic Industry
In industries where safety, compliance, and integrity are non-negotiable, packaging serves a far greater purpose than simple containment. The pharmaceutical packaging industry and the forensic sector both depend on highly secure, durable, and regulation-compliant packaging systems. From protecting life-saving medicines to preserving sensitive legal evidence, packaging plays a defining operational role.
Dhwani Polyprints, with its expertise in precision poly packaging manufacturing, supports these critical industries through solutions designed for strength, reliability, and consistent performance.
The Expanding Scope of the Pharmaceutical Packaging Industry
The pharmaceutical packaging industry has evolved rapidly in response to increasing global healthcare demand and stricter regulatory standards. Medicines today are distributed across regions and climates, making protective packaging essential to maintain stability throughout transportation and storage.
Pharmaceutical products must be shielded from moisture, oxygen, light exposure, and contamination. At the same time, packaging must carry accurate labeling, batch information, expiry details, and traceability codes. These requirements position packaging as a core component of pharmaceutical quality control rather than a secondary function.
As supply chains become more complex, the responsibility placed on packaging continues to grow.
Importance of Packaging in Pharmaceutical Industry
The importance of packaging in pharmaceutical industry is directly connected to patient safety and product effectiveness. Medicines are often chemically sensitive, and even minimal environmental exposure can compromise their efficacy. Protective polybags, sealed pouches, and high-barrier materials help preserve drug integrity from manufacturing facilities to end users.
Security is another crucial aspect. Tamper-evident seals and secure closures provide visible assurance that products have not been altered. This protects both the patient and the manufacturer from the risks associated with counterfeit or compromised medicines.
Regulatory compliance also highlights the importance of packaging in pharmaceutical industry. Pharmaceutical companies must adhere to strict guidelines related to labeling accuracy, traceability, and documentation. Reliable packaging ensures these standards are consistently met, reducing the risk of recalls or legal complications.
Beyond protection and compliance, efficient packaging improves storage, handling, and logistics. Strong, well-designed materials reduce the likelihood of damage during transportation, contributing to smoother distribution processes.
Materials and Manufacturing Precision
Pharmaceutical packaging demands materials that are non-reactive, contamination-resistant, and structurally durable. Polyethylene films, laminated pouches, and sealed protective bags are commonly used due to their high barrier properties and strength.
Dhwani Polyprints manufactures customized packaging solutions tailored to meet these demanding standards. With consistent thickness control, superior sealing strength, and strict quality checks, the company ensures packaging performs reliably under varied environmental conditions. By maintaining precision in production, it supports pharmaceutical brands in protecting both their products and their reputation.
The Critical Nature of Forensic Packaging
While pharmaceutical packaging protects products, forensic packaging safeguards evidence. The role of essential packaging for forensic industry lies in preserving integrity and preventing contamination. In legal investigations, even minor compromise can affect the credibility of evidence.
Forensic materials may include biological samples, documents, narcotics, or physical objects. Each type requires packaging that prevents cross-contamination and clearly indicates tampering. Packaging therefore becomes part of the evidentiary chain itself.
Because forensic evidence often passes through multiple departments before reaching a courtroom, durability and traceability are vital.
Forensic Packaging Solutions That Preserve Evidence Integrity
Effective forensic packaging solutions are designed with security and accountability at their core. Tamper-evident features ensure that once sealed, any unauthorized access is clearly visible. This protects the authenticity of the evidence and maintains legal credibility.
Contamination prevention is equally critical. Packaging must shield evidence from environmental exposure while preventing interaction between separate samples. Proper sealing mechanisms and strong material construction help achieve this objective.
Chain-of-custody documentation is another essential consideration. Packaging formats that allow clear labeling and tracking help maintain detailed records from collection to final analysis. This traceability strengthens the reliability of forensic processes.
By focusing on strength, clarity, and consistent manufacturing quality, Dhwani Polyprints supports organizations that rely on dependable forensic packaging solutions.
Compliance and Evolving Industry Standards
Both sectors are guided by rigorous regulatory frameworks. The pharmaceutical packaging industry must comply with health authority standards and Good Manufacturing Practices, while forensic departments operate within legal protocols that demand complete accountability.
Modern packaging solutions increasingly balance compliance with sustainability. Advances in recyclable poly materials and improved manufacturing efficiency allow companies to reduce environmental impact without sacrificing protective performance. As technology evolves, packaging continues to integrate better sealing techniques, stronger barrier properties, and enhanced tracking capabilities.
Safeguarding Health and Justice Through Reliable Packaging
The pharmaceutical packaging industry and forensic sector operate in environments where accuracy and reliability are fundamental. The importance of packaging in pharmaceutical industry is reflected in its direct impact on patient safety and regulatory compliance. At the same time, essential packaging for forensic industry ensures that evidence remains uncontaminated, secure, and legally admissible.
In both contexts, packaging serves as a silent but critical safeguard. Through its commitment to precision manufacturing and customized solutions, Dhwani Polyprints continues to support industries where protection, integrity, and trust are paramount.